Semiconductor & Advanced Laser · Scientific Instruments

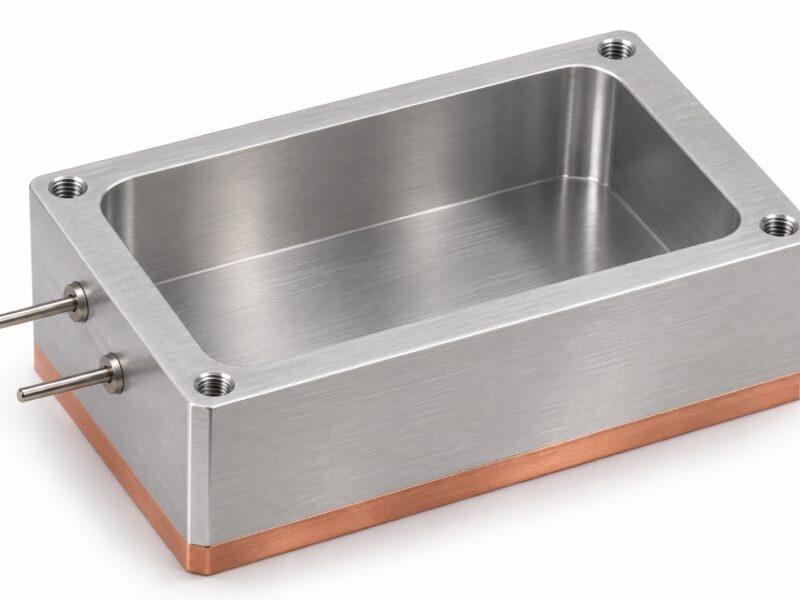
Precision Copper-Aluminum Brazed Housing

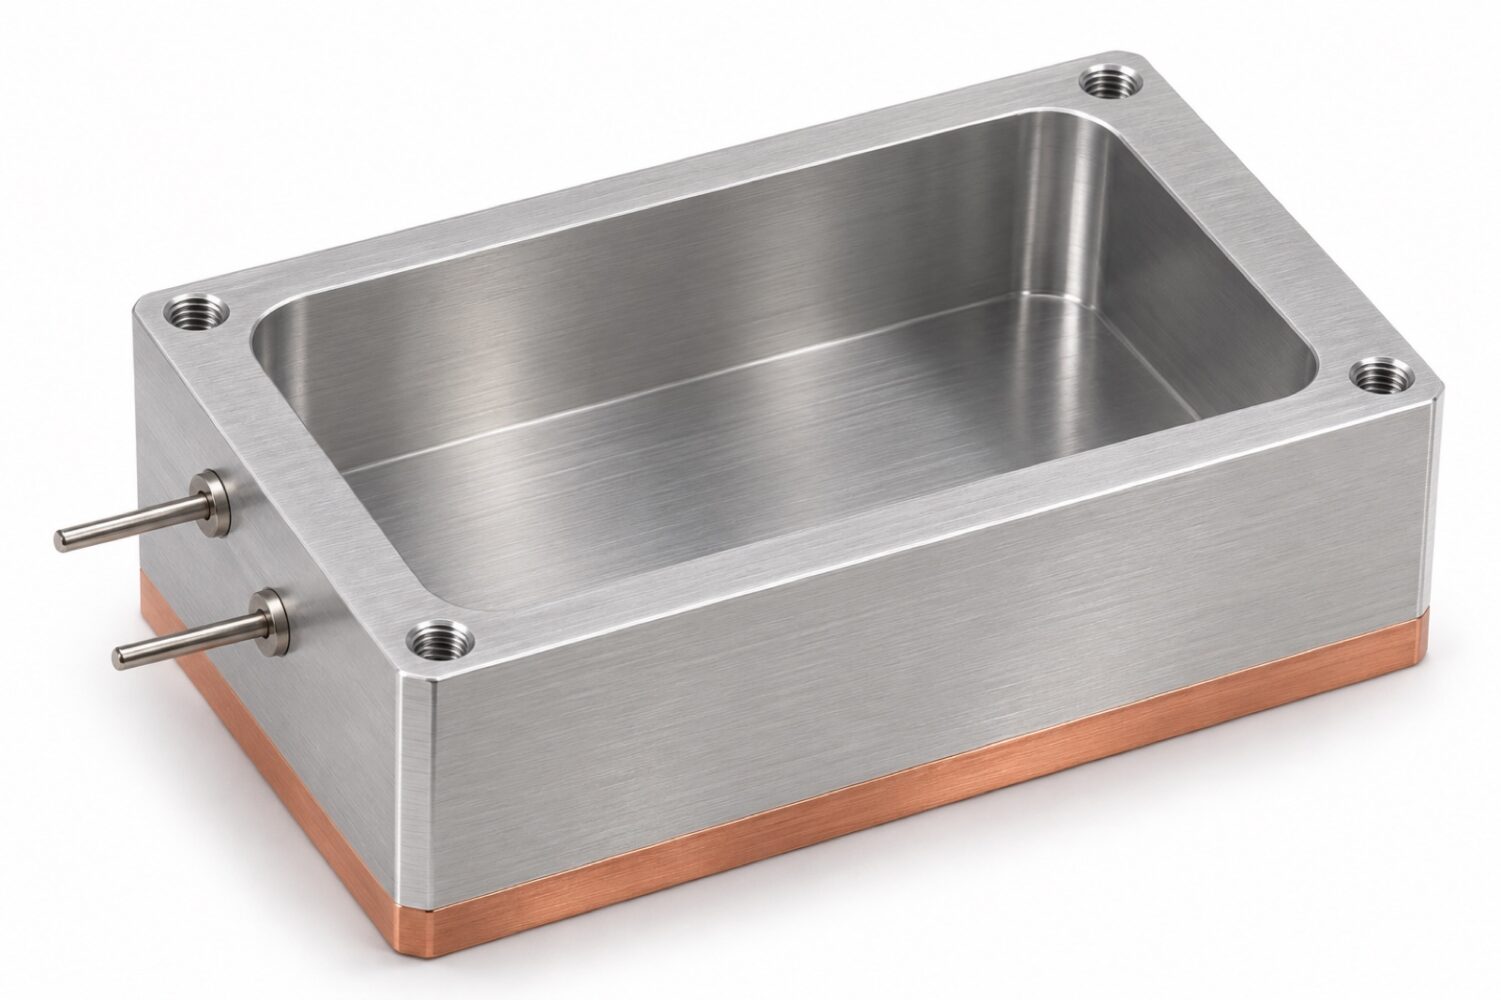
A copper base plate joined to a CNC-machined aluminium frame by a low-temperature process, combining copper's heat transfer with aluminium's low weight and machinability in a deep-cavity housing.

Client
A dissimilar-metal assembly development project
Tolerance
Flatness, cavity and mounting-hole position per drawing (checked after joining)
Inspection
Dimensional inspection (post-join) + joint / leak test where specified
Precision Copper-Aluminum Brazed Housing

The engineering story

From requirement to outcome

Join a copper base plate to a CNC-machined aluminium frame by a low-temperature process to form a deep rectangular housing with mounting interfaces and external pins, meeting drawing requirements after thermal processing.

Melting-temperature gap (~1,085 °C copper vs ~660 °C aluminium), tenacious aluminium oxide hindering wetting, thermal-expansion mismatch (~16.5–17 vs 23–24 ×10⁻⁶/K), brittle intermetallics at the interface, and a continuous rectangular joint whose seam appearance does not prove leak-tightness.

Qualified time–temperature profile with compatible filler; surface preparation and oxide management; fixturing and controlled thermal cycles to limit distortion; post-join dimensional checks plus joint and leak testing to the approved drawing.

Method: Dimensional inspection (post-join) + joint / leak test where specified

Tolerance verified: Flatness, cavity and mounting-hole position per drawing (checked after joining)

Geometry and function preserved through joining; critical dimensions, joint characteristics and sealing verified against agreed acceptance criteria.

Request a Quote

Have a similar engineering challenge?

Send the drawing and your requirement — we reply with a manufacturing approach and a quote.