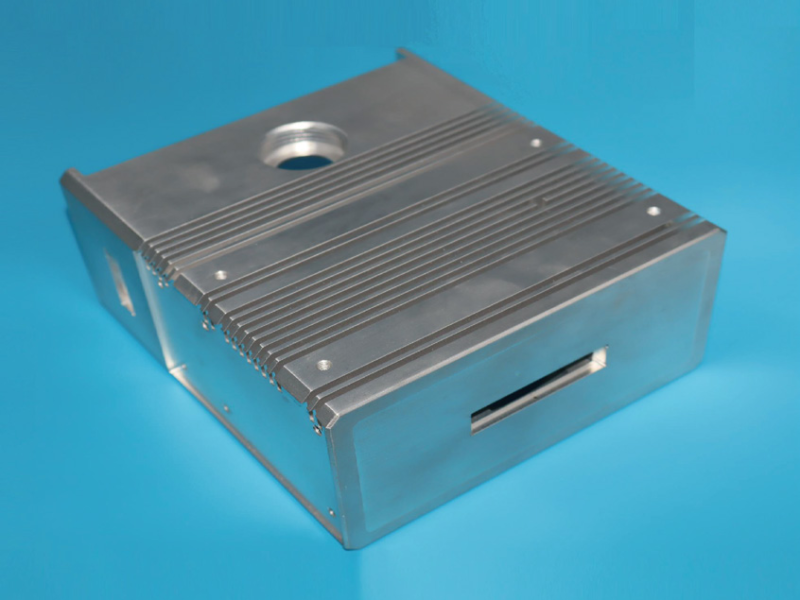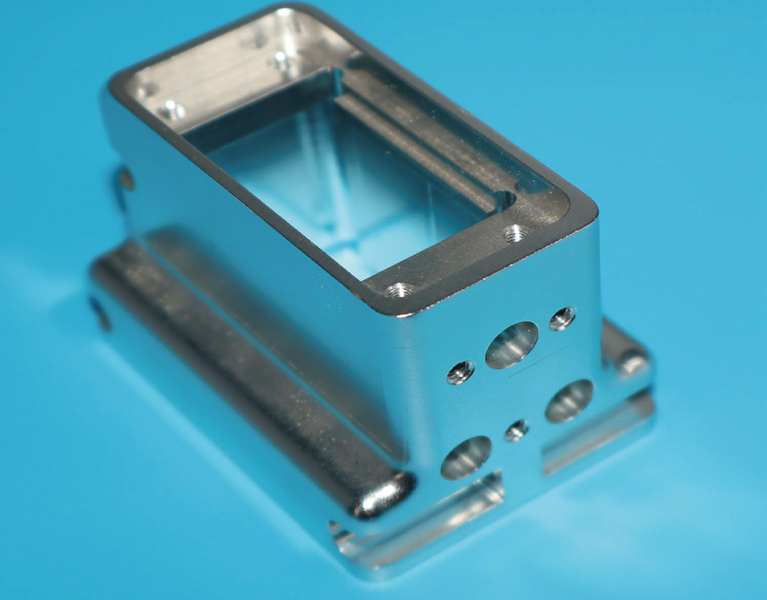

In one paragraph: CNC milling is the default — fastest and most economical for the majority of geometries and materials. Wire EDM earns its place when the material is hardened, the internal corners are finer than any endmill can turn, or the part must hold accuracy unattended over long cuts. High-end components are routinely both: milled for bulk material removal, EDM-finished where precision lives.
What each process actually does
CNC milling removes material with rotating cutters: 3-axis for prismatic parts, 4/5-axis for complex faces and undercut features. It is versatile, fast per volume removed, and works across nearly every machinable metal and plastic.
Wire EDM cuts conductive material with a charged brass wire, eroding a narrow kerf — like an ultra-precise band saw that does not touch the workpiece. Because there is no cutting force, hardness does not matter and delicate features survive.
The decision factors
Material hardness
Milling hardened tool steel above ~45 HRC is slow and tool-hungry; wire EDM cuts hardened steel and carbide as happily as annealed stock. If the part is heat-treated before final machining, EDM is often the natural finisher.
Internal corner radii
An endmill leaves a radius at least its own radius — typically ≥ 0.5–1 mm practical minimum. A 0.10–0.25 mm wire leaves internal corners an order of magnitude sharper. Sharp-cornered pockets, spline profiles and narrow slots are EDM territory.
Tolerance and surface finish
Both processes hold tight tolerances in capable hands. EDM’s advantage is consistency without force: no tool deflection, no workpiece distortion on thin sections, and excellent surface finish on hard materials where milling would need grinding.
Geometry type
Milling makes 3D surfaces, pockets and bores — anything with volume. Wire EDM makes through-profiles: punches, dies, plates, internal cutouts. Conventional (sinker) EDM extends the family to blind cavities and holes with spark-eroded finishes.
Cost and lead time reality
| CNC milling | Wire EDM | |
|---|---|---|
| Cost driver | Machine time, setups | Cut length × thickness |
| Thick plate with big pocket | Economical | Priced by kerf length — expensive |
| Hardened die insert | Difficult | Natural fit |
| Unattended overnight runs | Common | Classic strength |
Rule of thumb: if the feature could be made by either, milling usually wins on price; if the material is hard or the corners sharp, EDM wins on feasibility.
The hybrid workflow — where quality lives
A typical precision tooling or photonics part flows like this: mill the bulk geometry in the annealed state → heat treat → grind or mill datum faces → wire EDM the critical profile in the hardened state → finish and inspect. Each process does what it is best at, and the datums carry truth between them. Our shop runs both processes in-house under one quality system, so the handoffs are internal — capability benchmarks for both are published per process.
Quick chooser
- Soft/medium metal, 3D shapes, speed → mill it
- Hardened steel, carbide, sharp internal corners → wire EDM
- Blind cavity with fine detail, hard material → sinker EDM
- Both needs in one part → plan the hybrid from the start
Unsure which applies to your drawing? Send it — the process recommendation is part of the engineering review.